Square Bottle Labeling Problems: Wrinkles, Bubbles & Skew Fixed
The flat-bottle sibling of this guide: a seven-row symptom-to-cause diagnosis table plus the seven on-machine checks.
Labels climb and wrinkle on tapers because film cannot stretch: three fixes exist, ordered by cost.
A tapered face makes the upper edge of a label travel farther than the lower edge. Film cannot stretch, so it buckles; you see it as wrinkles near the shoulder and labels that climb out of position batch after batch. Three fixes exist, in rising order of cost: redesign the label to live only in the straight-wall zone (cheapest, changes your look); engineer a jig that holds the bottle at a compensated angle (our specialty, a one-time tooling cost, drawings archived for repeat orders); or choose machines that handle tapers natively: semi-automatic platforms with tapered fixtures, or automatic double-side machines with custom tooling. Send two bottles and your label art; the factory films the winning fix on your product within 48 hours.
Picture a label being pressed onto a cone. The bottom edge sits on a smaller circumference than the top edge. So when the label wraps, the top edge must cover more millimeters than the bottom edge. Pressure-sensitive film is designed not to stretch, and it keeps that promise by doing one of two things: buckling into wrinkles, or sliding upward toward where the circumference is larger. That sliding is “label climb”, and the buckling is the wrinkle band you keep finding near the shoulder.
The steeper the taper, the worse the differential. A woozy-style sauce bottle concentrates the problem at the shoulder transition, which is why the defect pattern is so consistent across brands using the same bottle. Nothing is “wrong” with the machine in these cases; it is being asked to lay a flat rectangle onto a surface that is not flat.
The useful concept from all of this is the straight-wall zone: the vertical band of the bottle where the surface is actually parallel. Whatever stays inside that zone applies like a cylinder: cleanly and repeatably. Whatever crosses it inherits the geometry problem. Every fix below is a strategy for keeping the label inside the zone, or compensating for the part that is not.
The cheapest fix costs a conversation with your label printer, not a tooling invoice:
When this works, it works perfectly, and it is permanent. The trade-off is design: your label gets smaller, and on a 5oz woozy bottle, shelf presence matters. That is why many brands skip straight to Fix #2.
When the label must stay as-is, an engineered jig (fixture) holds the bottle at a fixed attitude (often slightly tilted to pre-load the label against the taper), so application force enters the film along a controlled path on every bottle.
What a good tapered-bottle jig gives you:
This is our flagship capability: conical, oval, curved and bottom-face applications that standard machines decline. The engineering process and examples live on the custom labeling machine page, and the cost is a one-time tooling quote, not a per-bottle tax.
The front-and-back roller platform (T803) and the full-wrap platform (T805) both accept custom tapered fixtures, running 15–30 pcs/min at ±0.5mm. For most hot-sauce and cosmetic brands, this is the right machine: one operator, small footprint, and jigs that make the taper a solved problem. The class is detailed on the semi-automatic labeling machine page.
At line speed, the double-side class (60–120 pcs/min, ±1mm) takes custom tooling for conical faces, typically alongside square-bottle SKUs on the same machine. Expect the tooling conversation to include the fixture design we just described. See double-side labeling machines.
The benchtop electric front-and-back unit applies paired labels to round and wine-style bottles, and with the appropriate fixture handles woozy front/back pairs, a popular first machine for sauce brands. [Front/back/neck on one setup: confirm at engineering; TBC.]
The 5oz woozy bottle is the hot-sauce workhorse (dimensions vary slightly by supplier). Three labels compete for its surface:
Sauce brands are a steady share of the test-run video library; your bottle class is often already labeled on camera.
| Symptom on the taper | Cause | First fix to try |
|---|---|---|
| Wrinkle band near the shoulder | Label crosses the straight-wall zone | Shorten label height, or add the tapered jig |
| Label sits higher after each bottle | Climb: upper-edge length differential | Tilt-compensated jig; check web tension is not too high |
| Front and back at different heights | Paired heads out of datum | Re-zero both against one master bottle |
| Edge lifting at the bottom | Label touching the base curve | Raise label bottom edge; chamfer corners |
| Wrinkles only on soft bottles | Stiff film on squeezable container | Flexible face stock; see the design-side rules in the square bottle guide |
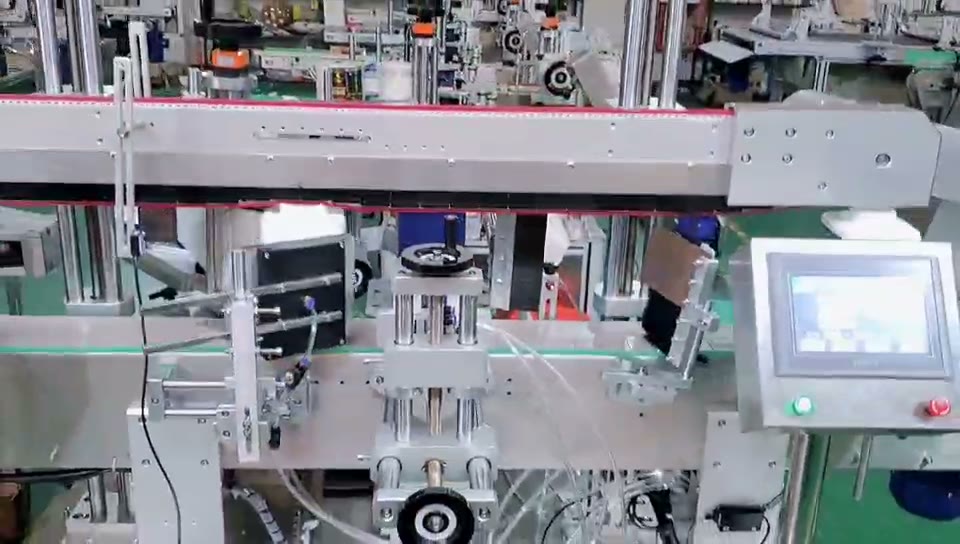
The same woozy bottle and label run free (wrinkles, climb), then in the tilted jig (clean wrap, repeatable height); both takes filed with the machine’s FAT documentation. Browse test videos or the FAT process.
Yes, with the right fixture. A standard round-bottle wrap setup will fight the taper; a machine fitted with an angle-compensated jig applies woozy bottles cleanly at 15–30 pcs/min semi-automatically, or at line speed on a tooled automatic. Send two bottles and your label art and we film the result before you buy.
The shoulder is where the surface stops being parallel, so the label’s upper edge must travel farther than the lower edge. Film cannot stretch, so it buckles into wrinkles. The fix is keeping the label inside the straight-wall zone (redesign), or compensating the geometry with a tilted, machined jig.
Try the label first if you have design freedom: a label living entirely in the straight-wall zone applies like on a cylinder, at zero tooling cost. If shelf presence requires the bigger label (common on hot sauce and cosmetics), the engineered jig is the answer. Both paths can be proven on camera in one test run.
Quoted per project: the price depends on bottle geometry, whether one or multiple bottle families share the jig, and the mounting platform. Drawings and bottle parameters are archived after the first build, so repeat orders are not re-charged for engineering. Send the bottle dimensions through contact & quote for a firm figure.
[TBC; front and back pairs are standard on the roller platforms with a paired setup; adding a neck/tamper-evident station depends on bottle geometry and layout, confirmed during engineering evaluation.] Declare all three labels at inquiry so the fixture and stations are designed together.
The flat-bottle sibling of this guide: a seven-row symptom-to-cause diagnosis table plus the seven on-machine checks.

Where tapered containers sit in the full machine map: types, prices and the 10 questions to ask any supplier.