
Label Cost per Bottle
OPP film labels typically cost a fraction of equivalent pressure-sensitive stock.
12,000–15,000 BPH rotary at ±1mm: OPP film and paper labels, servo feed to 100 m/min.
Pressure-sensitive (self-adhesive) labels carry their own adhesive: convenient, but the liner goes in the bin and the adhesive is in every square centimetre. An OPP film label carries no liner at all: the glue is applied only where needed, and only at the two ends of the label.
The result is the reason bottling lines have run hot melt for decades: OPP film labels typically cost a fraction of equivalent pressure-sensitive stock (commonly quoted at one-third to one-fifth per bottle at volume), and the machine applies glue to the two label ends only, so consumable cost per bottle stays low as speeds climb.
Whether the crossover has arrived for your line depends on volume, label design and SKUs. That arithmetic, with the honest counter-cases, is laid out in the hot melt vs pressure-sensitive TCO guide.
| Factor | Pressure-sensitive (self-adhesive) | Hot melt OPP |
|---|---|---|
| Label construction | Face stock + adhesive + liner | Face film only: no liner |
| Adhesive cost | In every label | Two glue strips per label |
| Typical label cost per bottle | Reference | Commonly 1/3–1/5 of PS at volume [TBC, confirm with your label design] |
| Best-fit volume | Low to mid rates, many SKUs | High rates, stable SKUs |
OPP film labels typically cost a fraction of equivalent pressure-sensitive stock.
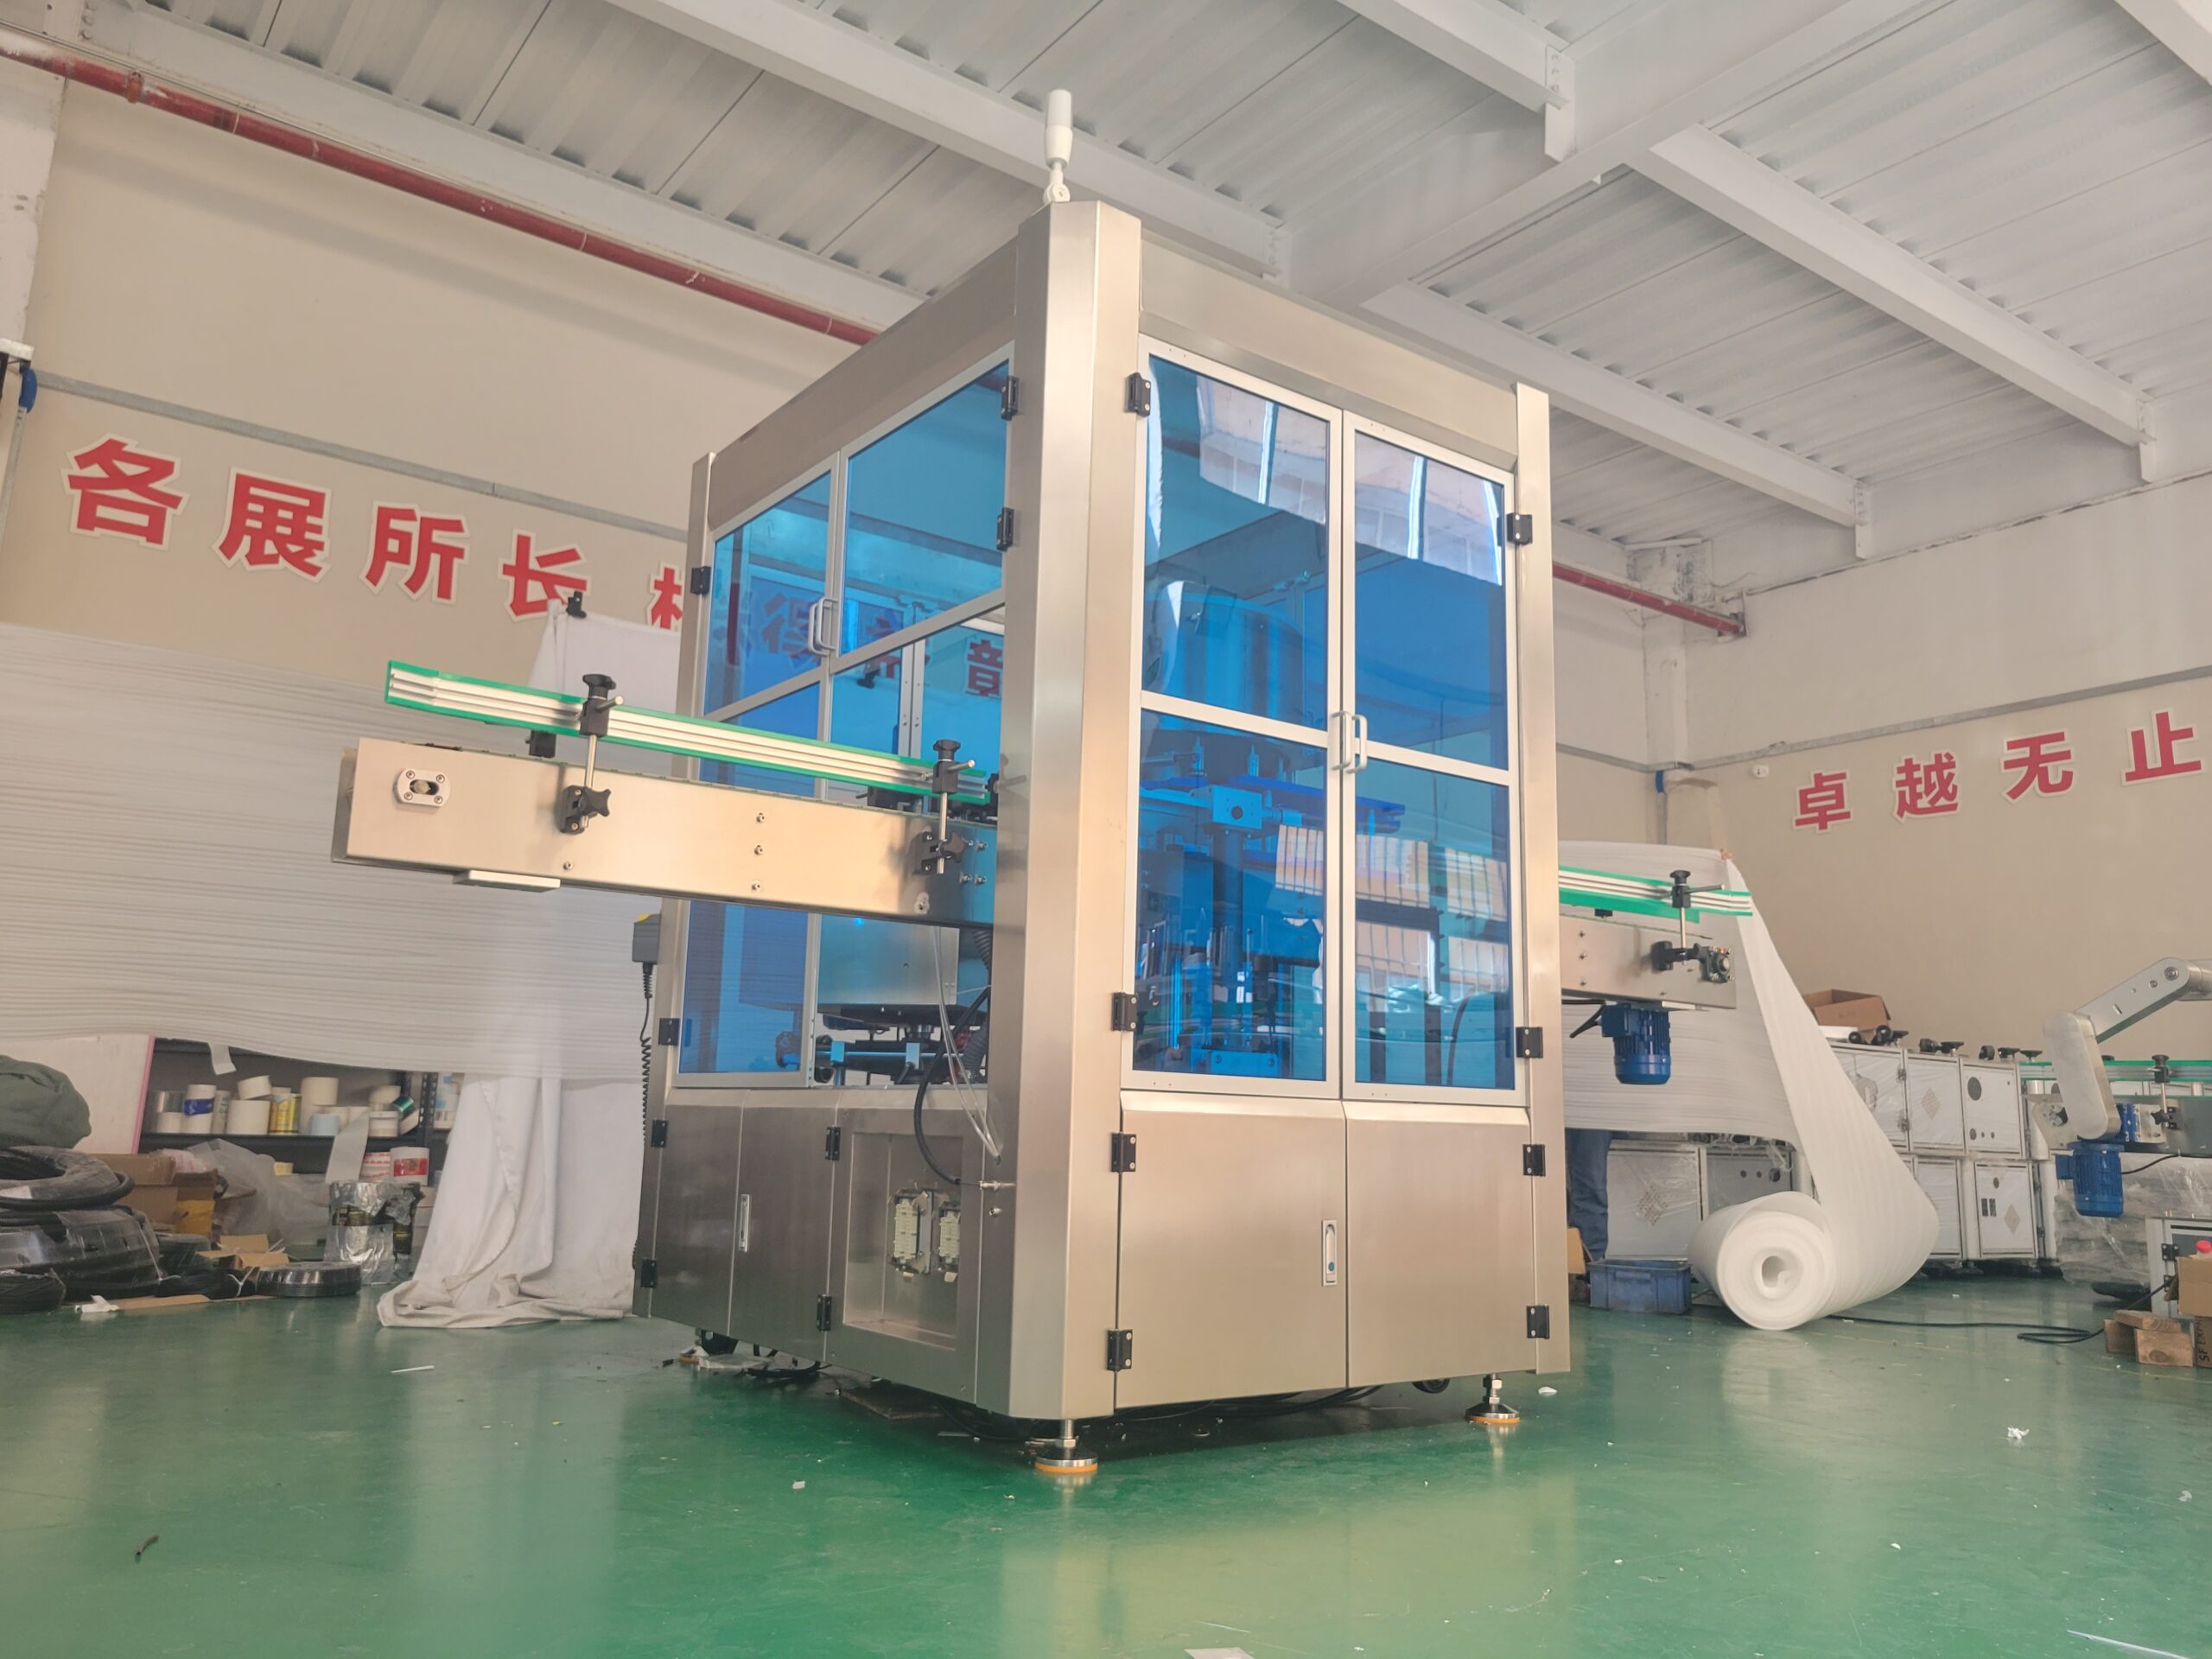
A rotating drum carries each bottle through the stations in precise registration. Vacuum and mechanical registration hold the container while the label is transferred, the reason a rotary holds ±1mm at rates a linear machine never attempts.
Hot melt adhesive is applied at 120–160°C to the leading and trailing ends of the label only. The glued ends bond to the bottle; the middle rides clean: no full-surface adhesive, no glue squeeze-out on the face.
The label reel is fed by servo drive at up to 100 m/min, cut to length and handed to the drum in sync with the bottles. Servo feed is what keeps label placement honest through reel changes and speed ramps.
The rotary 12-station configuration handles round containers φ40–80mm (the standard water, CSD and juice bottle band) at 12,000–15,000 bottles per hour.
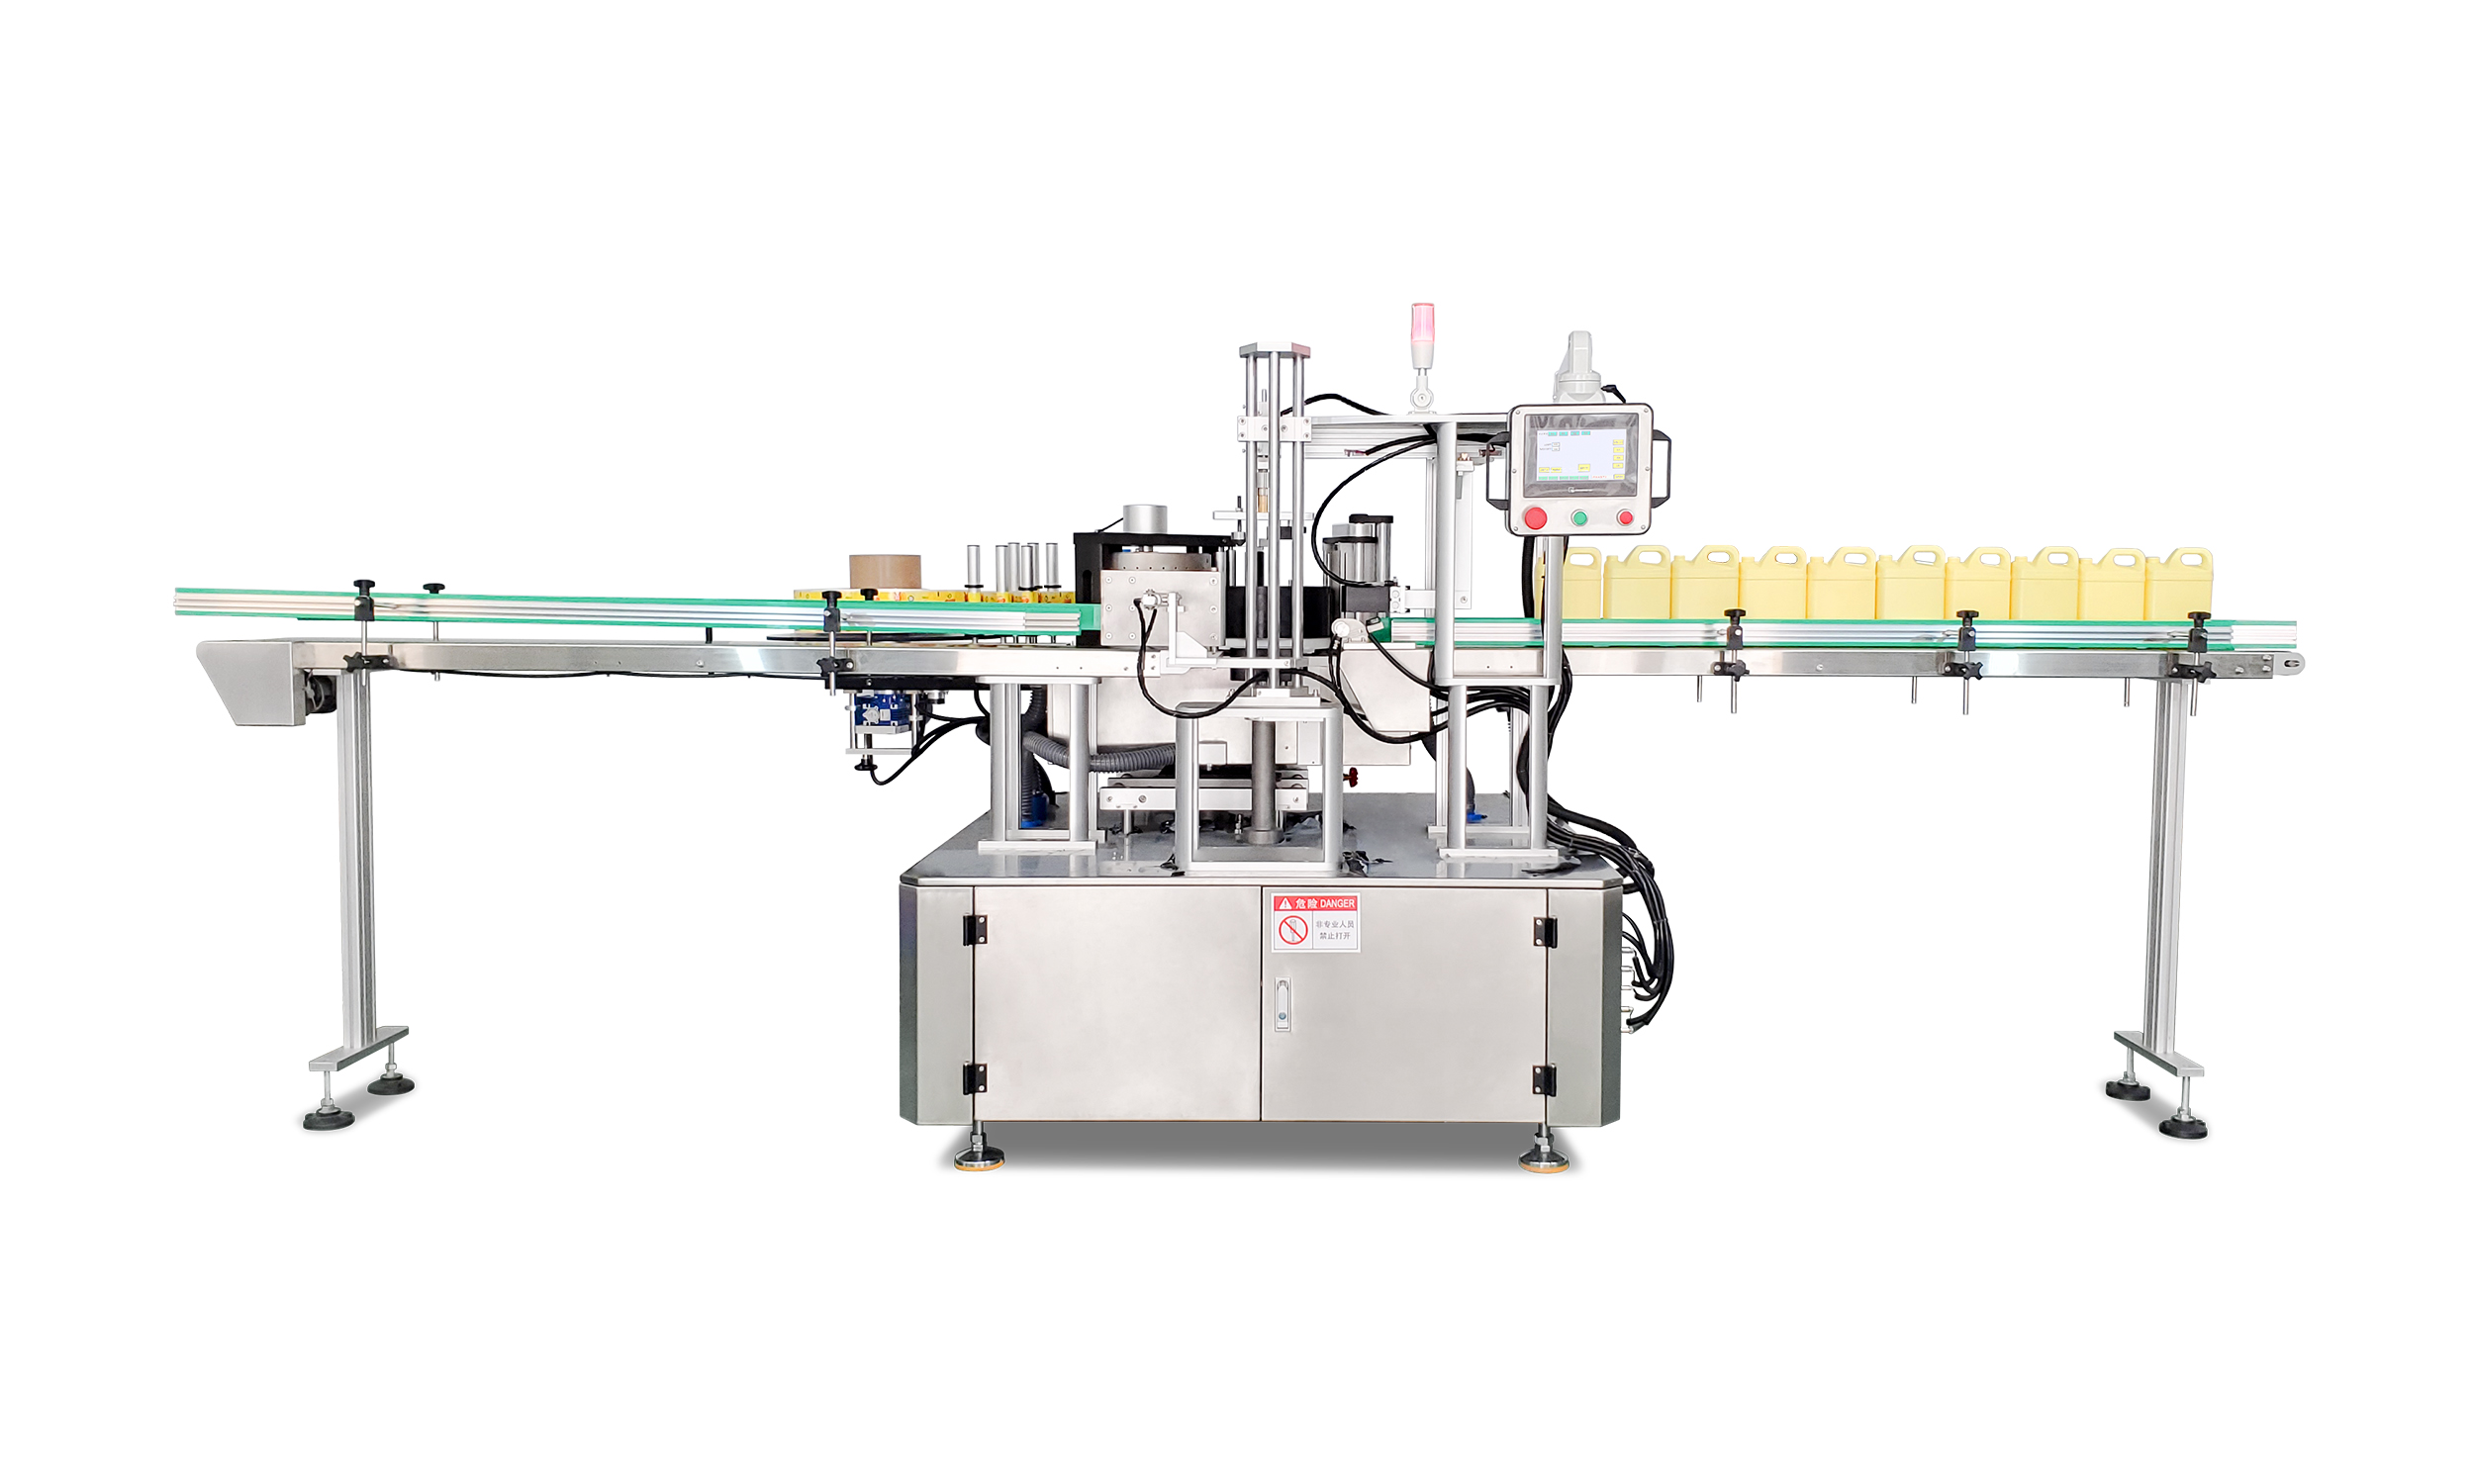
The headline machine: 12,000–15,000 BPH at ±1mm for φ40–80mm round containers.
The same drum logic expanded for oval containers: flask and oval-oval formats on a 16-station carousel.
Linear hot melt application for lower-rate lines and mid-size bottlers, configured by station count.
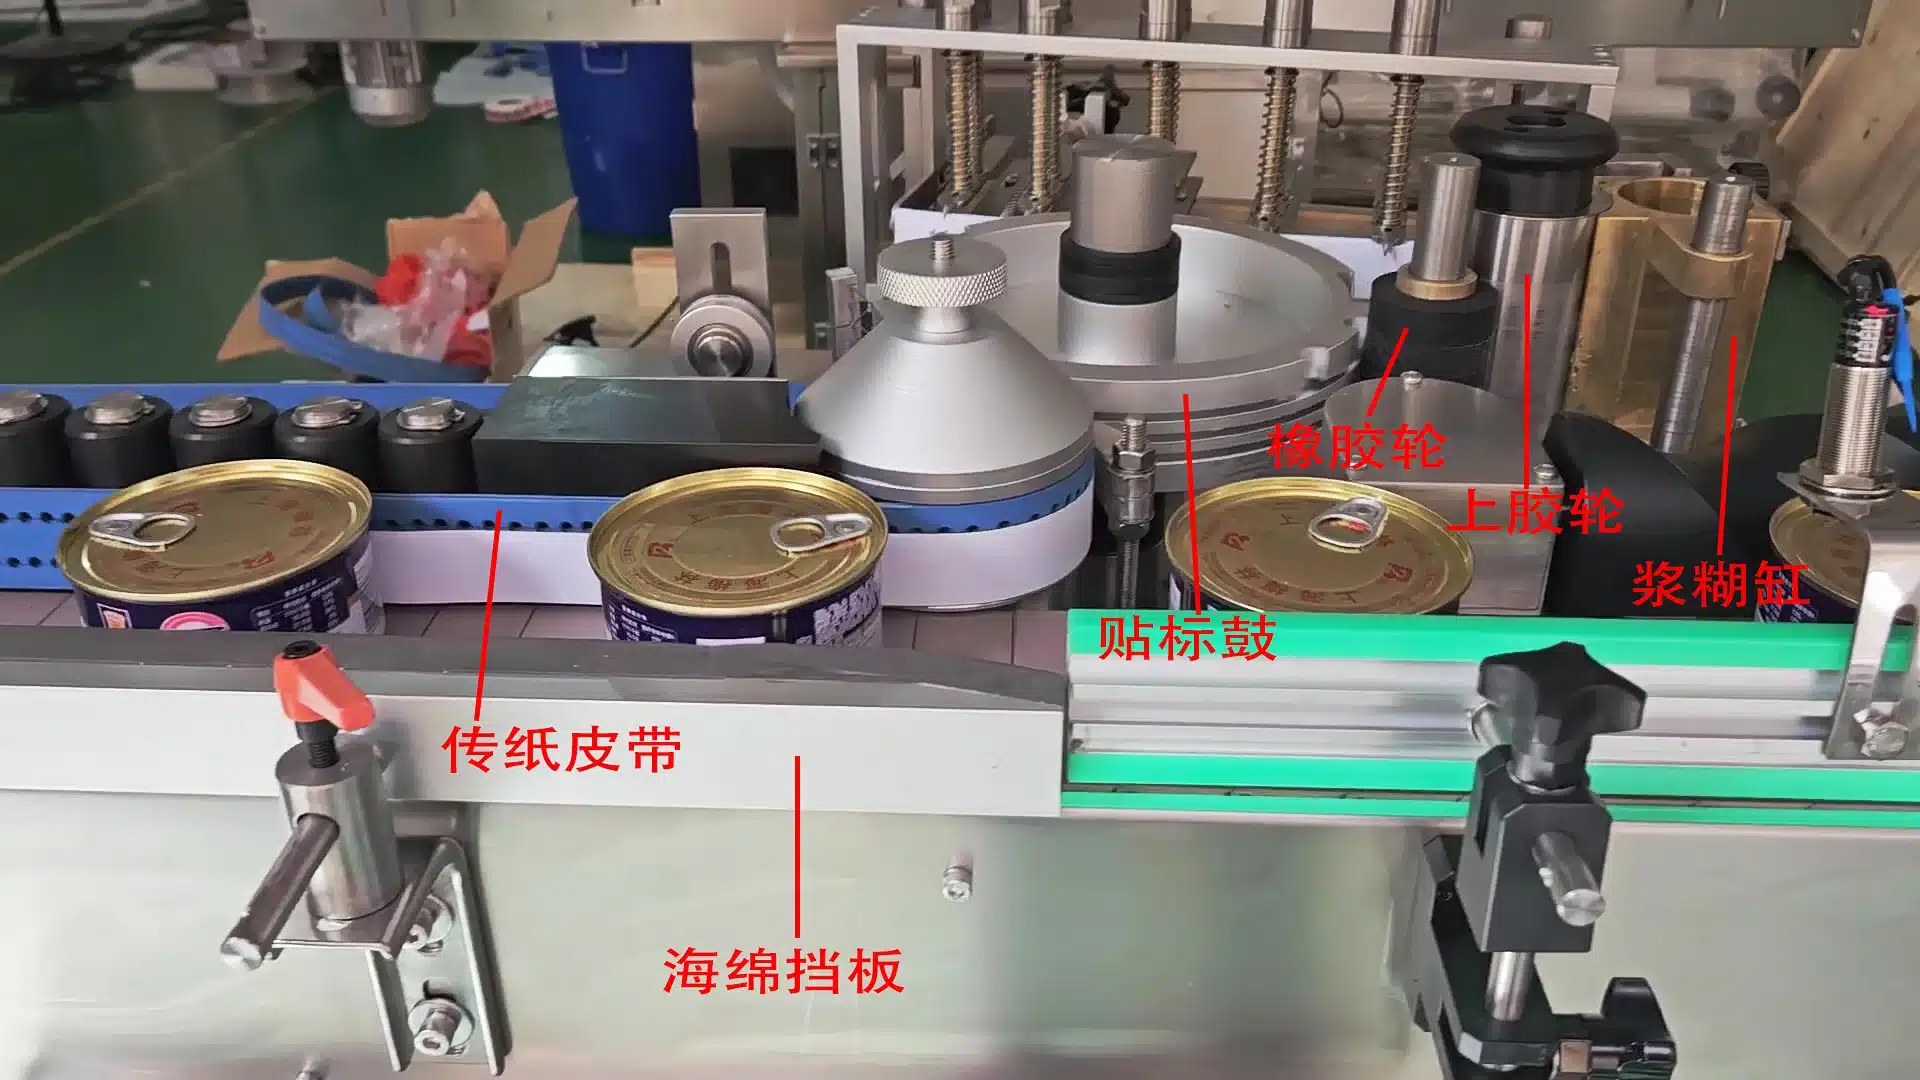
Traditional paper-label economics for cans and bottles, in live production at a Russian brewery customer’s plant.
| Parameter | Value |
|---|---|
| Throughput | 12,000–15,000 bottles/hour |
| Accuracy | ±1mm |
| Bottle diameter | φ40–80mm (round) |
| Label L × W | L 20–430 × W 20–140mm, OPP film, paper & paper-plastic composite |
| Glue temperature | 120–160°C, applied at both label ends only |
| Servo label feed | Up to 100 m/min |
| Main frame | 1650 × 1350 × 2100mm |
| Power | 3-phase 380V · 8000W |
| Weight | ≈2,000kg |
Specifications from the factory datasheet; 16-station and inline variants configured per line.
The crossover sits at volume. Around the 8,000 bottles-per-hour mark (the level industry consensus keeps landing on), OPP’s lower per-bottle label cost starts to outrun pressure-sensitive’s flexibility; below that, PS machines and their simpler operation usually win on total cost. Above it, every month of PS labeling is money spent on liners.
Hot melt also owns specific physical niches regardless of rate: full-body OPP decoration on PET bottles, and hot-fill beverage lines where wrap labels must survive heat that loosens pressure-sensitive adhesive. Beverage-scale economics in detail (including the counter-cases where PS still wins) is the subject of the hot melt vs PS TCO guide.
Where we fit: we build the mid-capacity rotary band (12,000–15,000 BPH) that sits between benchtop PS automation and the giant beverage OEMs who won’t quote below their minimum line sizes. See how it pairs with the rest of the range on the beverage, wine & brewery page.
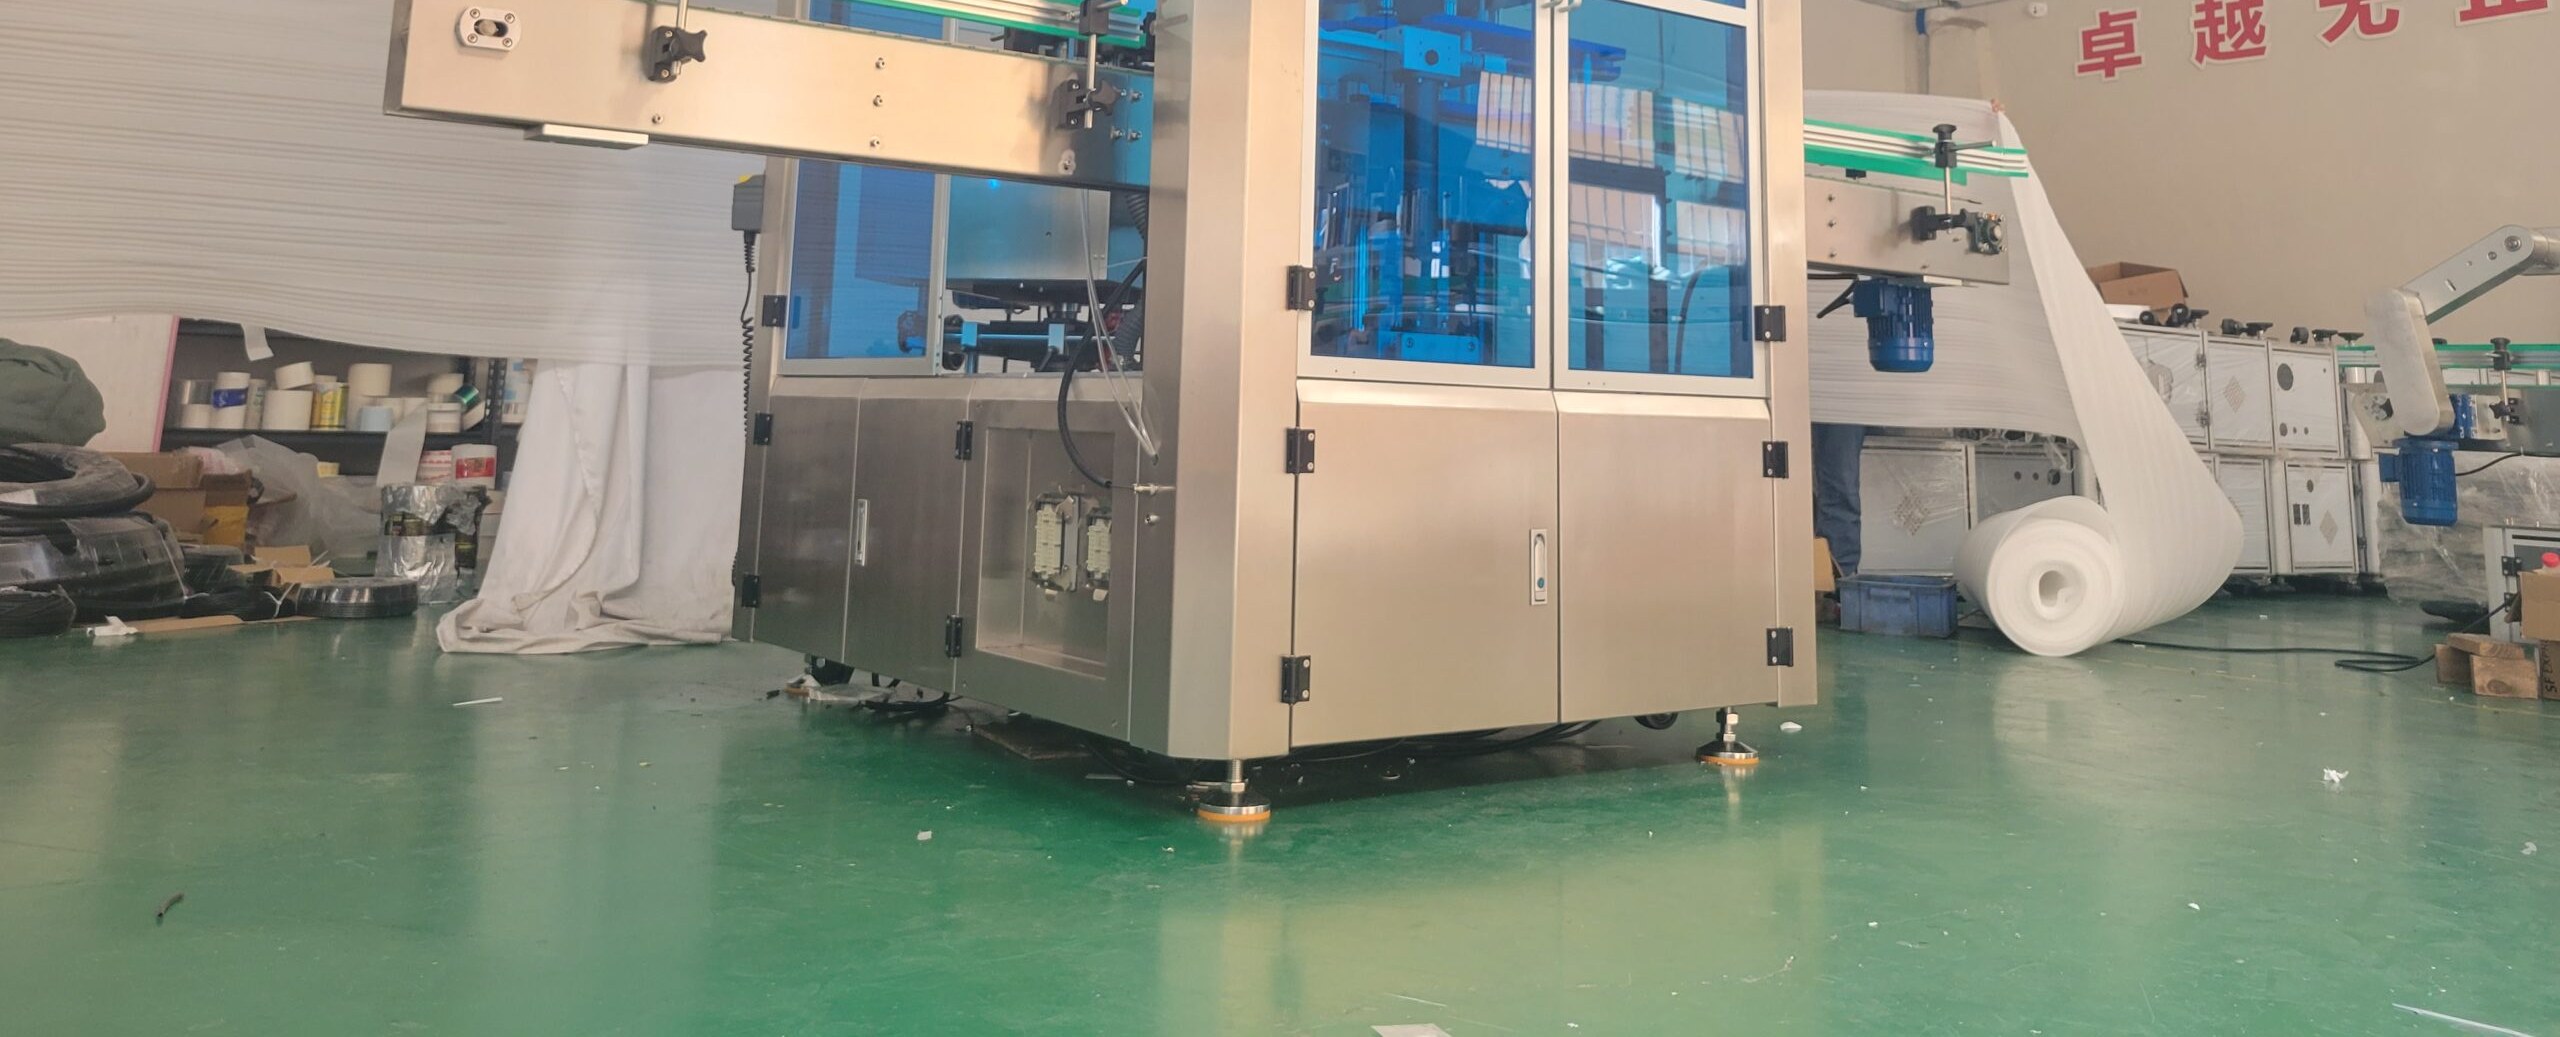
The melter holds and heats the adhesive to 120–160°C and feeds the application heads; capacity and hose layout are matched to the station count at engineering: inline units integrate compact melters, the rotary carries its own.
Consumption is a function of glue-strip length and label count. Because gluing is confined to the two label ends, grams-per-bottle stays low relative to full-coat systems. Exact per-1,000 figures depend on label size and glue pattern [TBC, quoted with your label design].
Label reel changes are servo-assisted for fast splices; glue-path cleaning follows the adhesive supplier’s hot-flush procedure at scheduled intervals. We document the maintenance rhythm in the English manual and training video shipped with the machine.
A 2-ton machine is accepted like a benchtop: your bottles at full speed on video; the FAT process gates shipment.
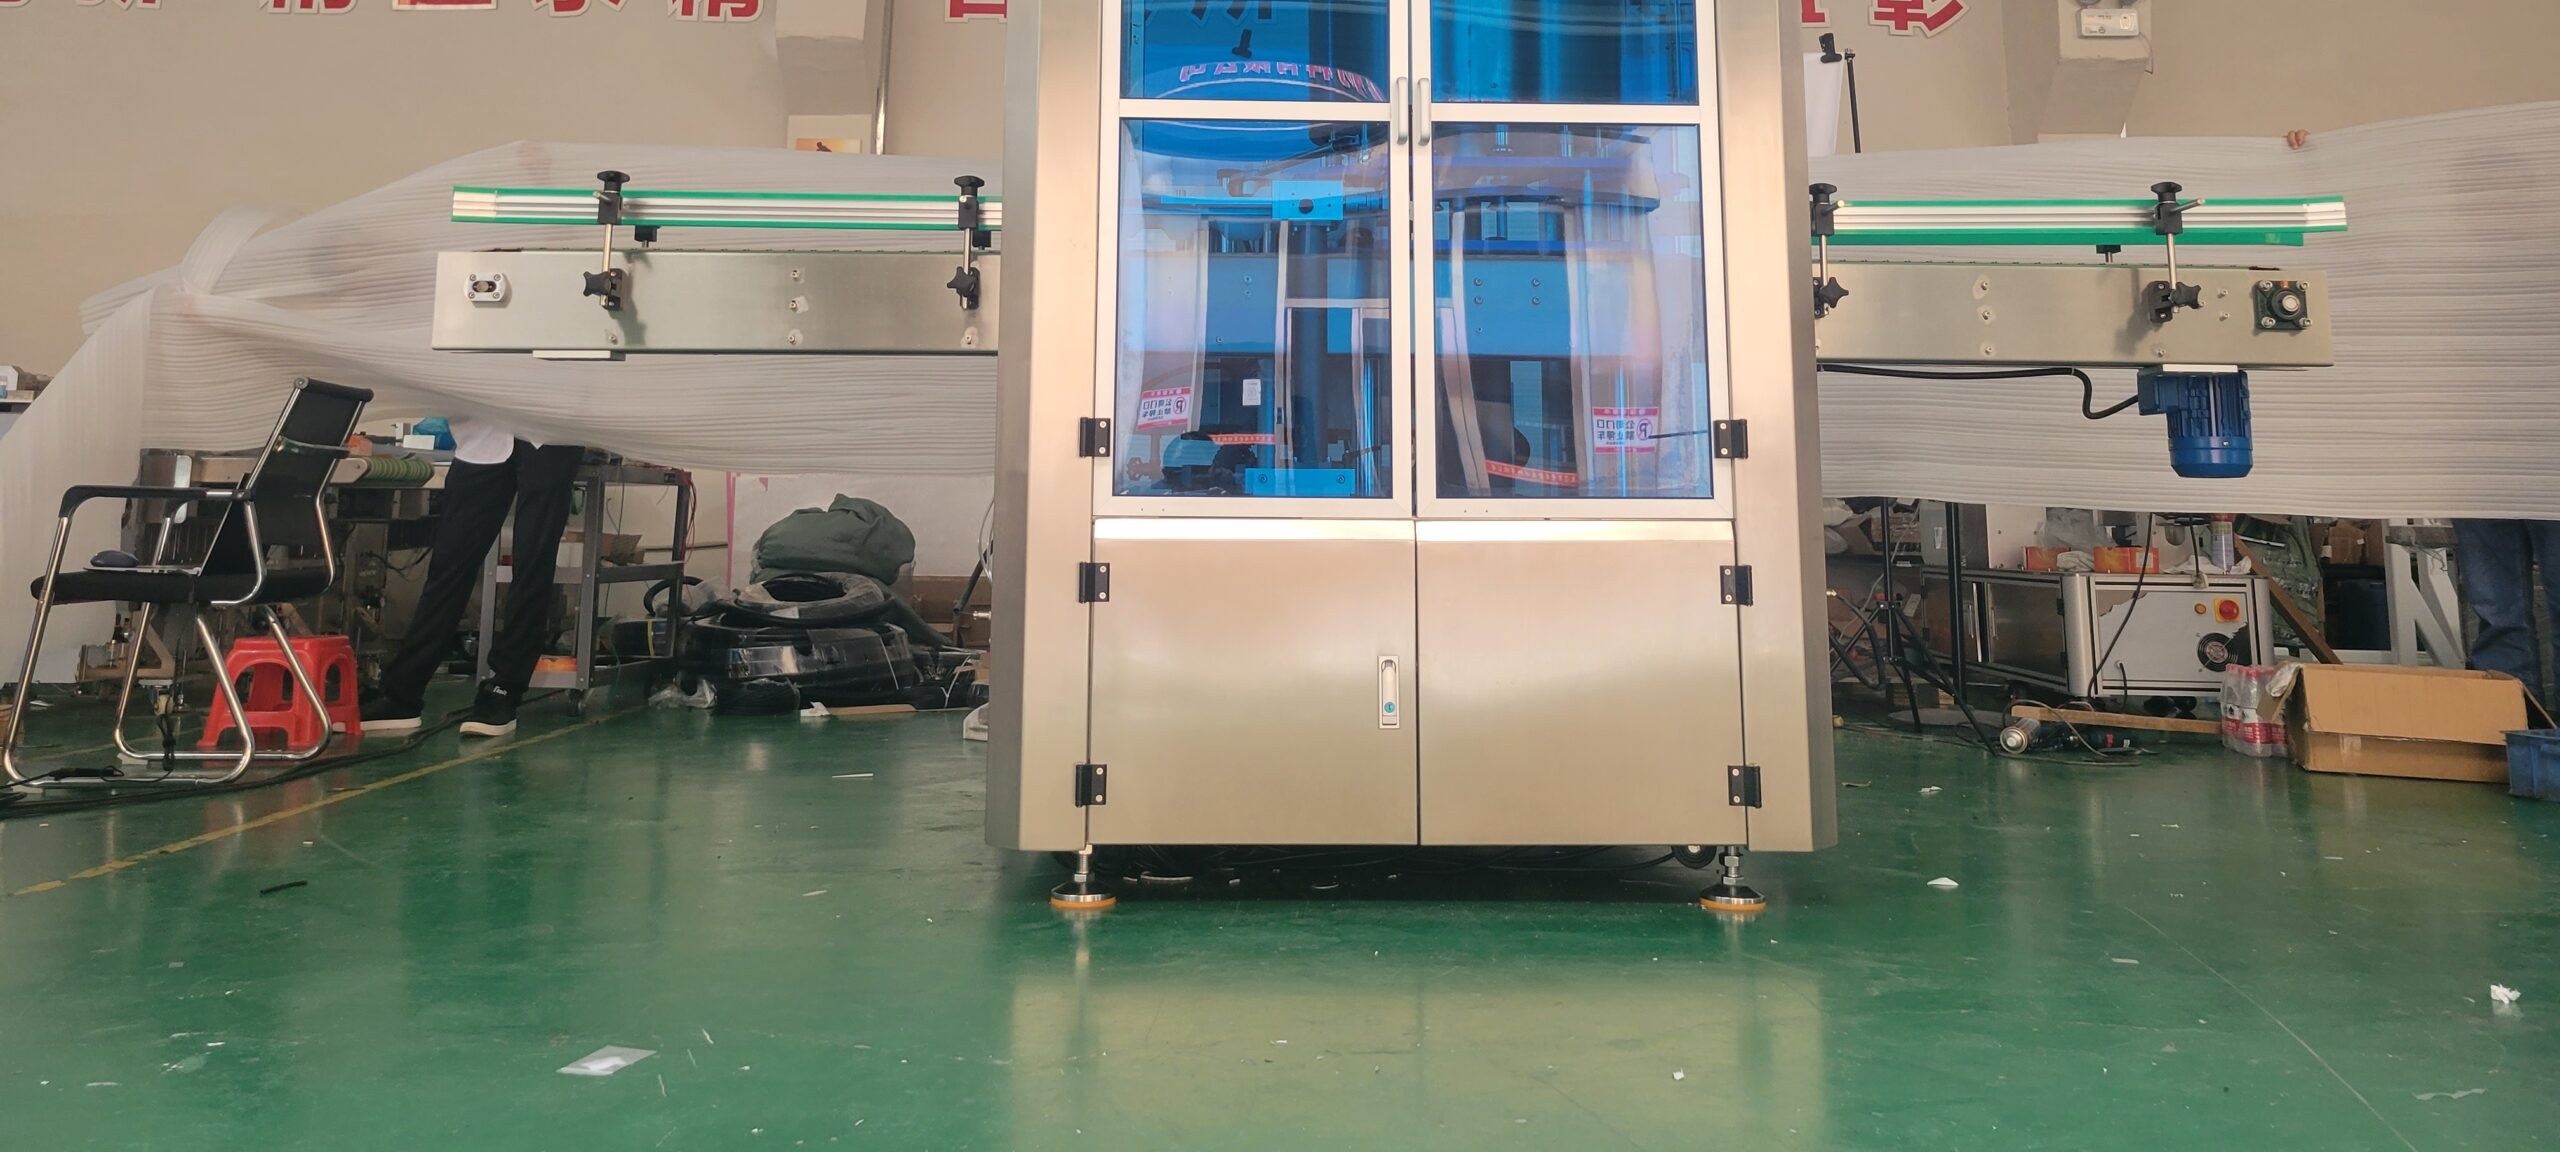
From $25,000 baseline. The rotary 12-station and its variants are built to order, so the final figure follows your bottle, label, glue system and line speed. The engineered proposal includes line layout and cost-per-bottle modeling before any commitment.
Around 8,000 BPH is where industry consensus places the crossover: below it, pressure-sensitive usually wins on total cost and flexibility; above it, OPP’s liner-free label economics take over. The full decision model (including hot-fill and full-body cases) is in the hot melt vs PS TCO guide.
The rotary 12-station handles round bottles φ40–80mm with labels L 20–430 × W 20–140mm. Materials: OPP film, paper and paper-plastic composites: the liner-free family that hot melt was built for. The 16-station variant covers oval bottles.
Consumption depends on label size and the glue-strip pattern. The system applies adhesive only at the two label ends, not across the face, which keeps grams-per-bottle low. Exact per-1,000-bottle figures are quoted with your specific label design [TBC].
Yes. Hot-fill PET is one of hot melt’s natural niches: the glue bond survives fill temperatures that loosen pressure-sensitive adhesive, and full-body OPP decoration conforms to the PET profile. Confirm your fill temperature and bottle geometry in the engineering evaluation.
The machine is built to order, then accepted via live video FAT with your team before shipment. Shipping and installation for a ≈2,000kg, 3-phase 380V machine (rigging, utilities and site prep) are scoped per project [TBC]. The proposal covers layout, power and the delivery timeline.